Decades of Experience. Continuous Improvement.
Why Vincent Continues to Improve the Shredder
Industrial shredder design is only as good as its performance in the real world. Over the years, Vincent Corp has continued to refine its shredders based on engineering experience, customer applications, and lessons learned from equipment in the field.
Materials behave differently, and the demands placed on a shredder can vary significantly from one application to another. As Vincent Corp has gained experience, we have looked for ways to improve material flow, capacity, durability, maintenance, and overall productivity.
Some changes have been major design improvements. Others have been small refinements that solved a specific problem or made the equipment easier and less expensive to build and maintain.
This history of continuous improvement is an important part of the Vincent approach: listen to what the equipment and the customer are telling us, learn from it, and use that knowledge to build a better shredder.
That philosophy has shaped the Vincent shredder through several generations of design.
The Early Years: Merging for Improvements
Vincent started making shredders in the 1930’s, to improve the capacity of the dryers we operated (making cattle feed out of orange peel). In 1968 the Rietz company merged with Vincent. They took our screw press designs, and we dropped our vertical shredder in place of their Rietz RD-18, which is a much better vertical shaft shredder. That deal soon fell apart, and Vincent resumed making their own shredders (or hammer mills).
Learning from Experience — The Move to Horizontal Shafts
Vincent’s early shredders used vertical shafts. Field experience revealed a significant maintenance problem: the lower bearing was exposed to liquid from the shredded material. That experience eventually led Vincent toward a horizontal-shaft design.
From Citrus Feedmills to Shredders
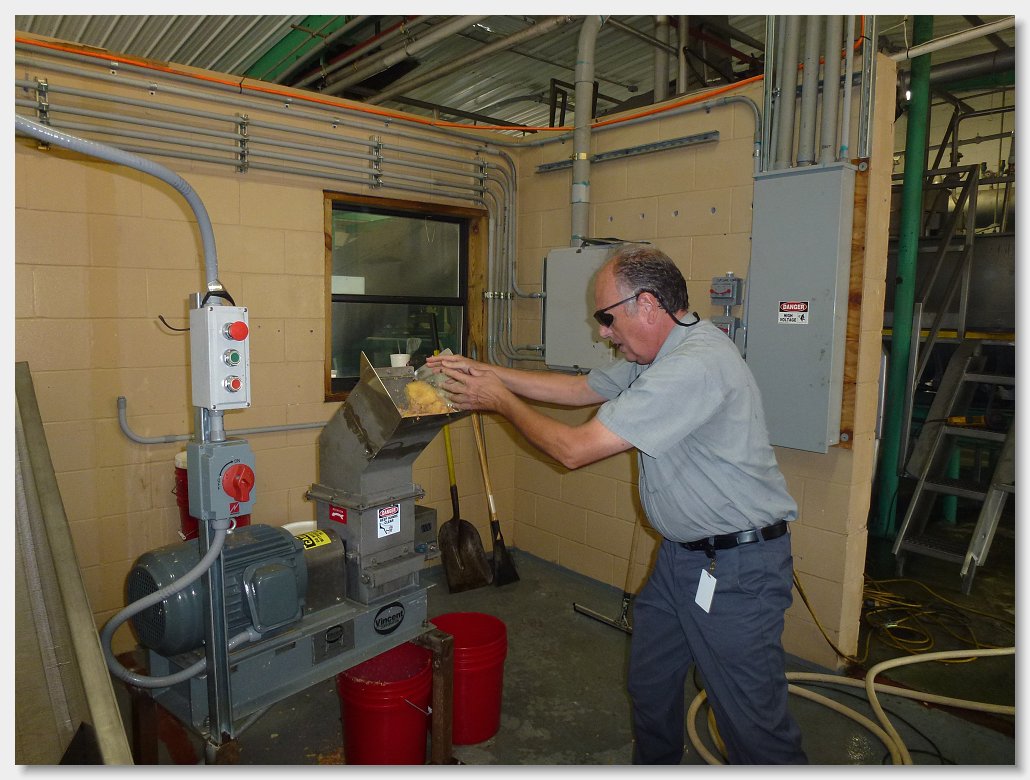
These new horizontal shredders were designated Series VS, for Vincent Shredder. We have two versions of these shredders: thin blades and thick blades. The thin blades were used to slice lime and lemon peel in pectin peel washing operations. The thin blades were susceptible to damage from tramp metal. Thick blades hold up better to tramp material and are used in shredding orange peel to make cattle feed.
The VS Series — A More Practical Shredder Design
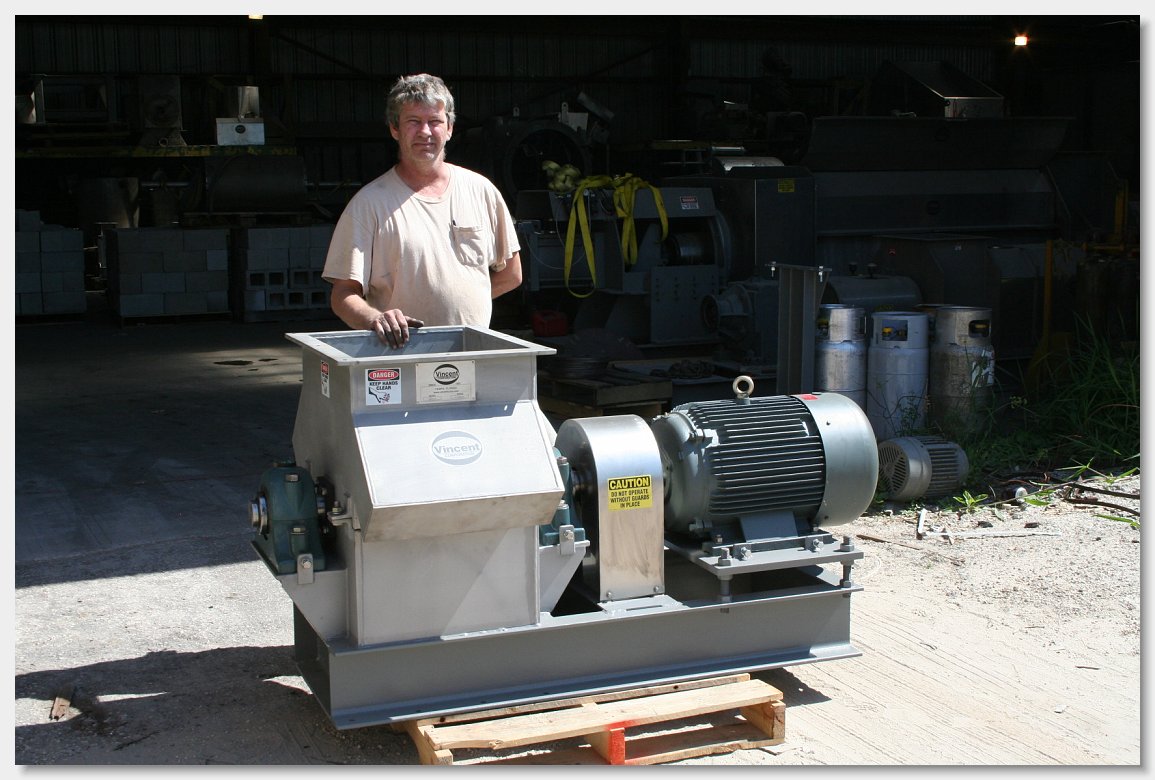
Vincent Corporation’s experience with earlier shredder designs led to a significant change in the way the machines were built. The VS Series introduced a horizontal rotor, addressing several of the maintenance and operating challenges associated with the earlier vertical-shaft designs.
With the rotor positioned horizontally, the lower bearing was no longer exposed to material and liquid passing through the shredder. This made the machine easier to maintain and better suited to the wet, fibrous materials commonly encountered in food-processing applications.
The horizontal design also provided a practical foundation for further improvements to the shredder. Over time, Vincent refined the rotor arrangement, material inlet, drive system, cutting configuration, and other components based on experience with different applications.
The VS Series became the foundation for the Vincent shredder designs that followed—and the design continues to evolve today.
The VCS Series — Adding the Comb Concept
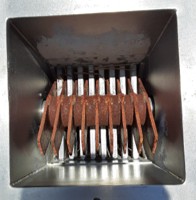
Vincent Comb Shredder. The blades of the rotor fit between fixed teeth. These fixed teeth form a grill or comb. They run from one side of the housing to the other. As the blades of the rotor spin, there is a scissors action, slicing the material. (There is no screen.)
Most VCS comb shredders operate without the comb being used, just doing a rough pre-breaking. This is because the main trouble with the comb shredder occurs when a piece of heavy tramp metal enters the machine. The rotor will jam and stop so suddenly that inertia of the rotor will break the cast iron housings of the pillow block support bearings. We have found that the VCS shredders work well, in many applications, without the comb. They do an adequate job of breaking up material so that it will effectively pass into a screw press.
Design Improvements Driven by Experience
90° → 180° rotor spacing
Not many years ago we found that the shredders work better if the blades are 180 degrees apart instead of 90 degrees. We made them 90 degrees for decades, thinking they would be better balanced. However, it turns out that balance is not affected. What does happen is that capacity goes up because there is a longer interval between blades swinging past the inlet, so material falls deeper into the shredder before it is hit by an oncoming blade.
Today we make all our shredders with blades 180 degrees apart. Discussion with Corenco, a shredder specialist company, gave us the confidence to make this change.
Inlet Redesign
The inlet hopper of the shredders used to be the width of the rotor by one half of the diameter of the rotor. That is, it was a rectangle located over one half of the rotor. The idea was that the rotor would turn so that the material, which all fell on one side of the rotor, would be thrown down toward the discharge of the shredder.
About ten years ago we found out that it works fine if there is a square inlet to the shredder, measuring the width of the rotor by the diameter of the rotor. This design does tend to throw material up and out of the shredder, so we always expect that there will be something to stop this material from flying out. This “something” would be the cover over a screw conveyor which carries material to the shredder, or a dog-leg chute over the inlet to the shredder.
This square inlet is less expensive to manufacture. Also, it eliminates the job of removing a worn rotor from the shredder and turning it 180 degrees around.
Reversible Rotation
Ironically, we had some models where we ran the rotor in reverse, so that the tendency was to throw most of the material up and out of the shredder. This arrangement suited certain applications.
- Added bonus of Reversing Directions: We used to have to remove a worn rotor from the shredder and turn it 180 degrees around to use the other (non-worn) edges of the rotor hammers. Now, when the teeth are worn on one side, it is necessary only to switch two of the electrical leads going to the motor, reversing the direction of rotation. A Florida engineer, David Tegreene, was the first to come up with this.
Bearing Arrangement
On the larger 18″ models we use one expansion pillow block bearing and one non-expansion pillow block bearing to support the rotor. The non-expansion bearing goes in the inboard position, closest to the coupling. The rotor does not expand from heat, but it can move from shock and distortion. This allows us to lock one end of the rotor and let the other float.
Coupling Design
The 18″ shredders use Dodge ParaFlex couplings between the motor and rotor. This keeps shock from the rotor from being transmitted to the motor. The ParaFlex is like the tire of a small car. One rim is clamped to the rotor shaft and the other rim is clamped to the motor shaft. These are rather expensive, but they are the best coupling for the application.
Tramp-metal protection
It was common practice to put metal traps on the side of the shredder housing. These would fill up with the material being shredded, which was soft material. When a piece of tramp metal or a rock came along, the idea was that it would be thrown into the trap or pocket on the side of the housing. This tramp material would imbed itself there, to be removed periodically. Today we generally do not bother putting these traps on our shredders.
Note that with the original rectangular inlet, there was need for a trap on only one side. With the square inlet, two traps were needed since the machine could be operated with the shredder going in either direction of rotation.
Fixed vs. pivoting cutting elements
There are some shredders or hammer mills built where the hammers are held by a single pin between two plates. These hammers can pivot when they hit the material being shredded. Vincent never did this. All of our shredders have had hammers or blades that are rigidly mounted to the shaft. This rigidity was achieved by either using two pins between parallel plates to hold the blades or by welding or keying the blades to a shaft. Today we almost always use keyways to hold the blades to the shaft.
Where the blades were welded to the shaft, the construction consists of a tube which is slipped over the shaft. The blades are welded to this tube. The tube shrinks from the welding operation, firmly gripping the shaft. In this manner stress risers, from the welding, are avoided in the shaft.
Vincent makes blades or hammers out of a 410 series stainless. This alloy is used because it can be hardened by heat treating.
Drive System Evolution
Vincent has used both belt-driven and direct-coupled drives over the years. The larger 18-inch shredders operate at 1,800 or 1,500 rpm, while the 12-inch and 8-inch models operate at 3,600 or 3,000 rpm.
Earlier machines were often equipped with belt drives between the motor and rotor. One advantage of the belt drive was that it provided some protection if the rotor became jammed while operating.
Today, Vincent uses direct-coupled motors because they are less expensive to build while providing a straightforward, compact drive arrangement. The evolution from belt drives to direct coupling is another example of how Vincent has refined the shredder design based on experience and practical considerations.
Designed Around the Application
Vincent Corp has years of experience with hundreds of different applications. Each trial teaches us what does work, what doesn’t work, and what could be improved. When you have an application that you want dewatered you are partnering with the experts at Vincent Corp to tailor make it efficient for your specific application.
Continuous Improvement, Built on Experience
Vincent’s shredder designs have evolved through decades of engineering experience, field experience, and a willingness to change when a better approach is found.
From the early vertical-shaft machines to today’s horizontal-shaft VS and VCS shredders, each generation has incorporated lessons learned from real applications. Changes to rotor configuration, material flow, maintenance, drive systems, and other components have been made to improve how the equipment performs with different materials and operating conditions.
That process continues today.
Vincent works closely with customers to understand their materials, production requirements, and processing challenges. The shredders used for citrus waste, pineapple juice, and produce waste have been optimized for their industries.
That experience helps us configure equipment to meet the demands of the application—not simply reproduce a standard design.
Better equipment starts with understanding the application.